Introduction
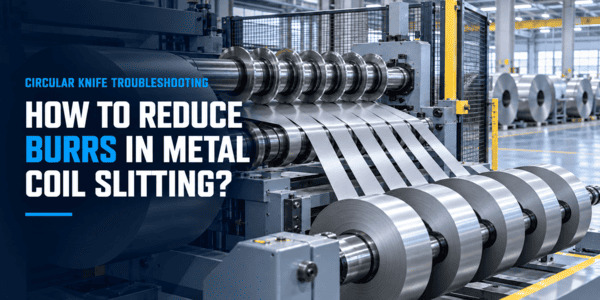
Burrs on slit metal edges can damage downstream tooling, interfere with welding or forming, create handling hazards and increase scrap. When burr height begins to rise, operators often replace the circular knives immediately. A dull edge may be involved, but the blade is only one part of the slitting system.
In rotary shear slitting, an upper and lower circular knife initiate deformation and guide the strip toward a controlled fracture. The final edge normally contains rollover, a bright burnished zone, a darker fracture zone and a small burr. The goal is not to chase an unrealistic “zero-burr” condition in every material; it is to keep the burr within the customer’s specification and consistent across every lane and throughout the coil.
Quick...



 English