Introduction
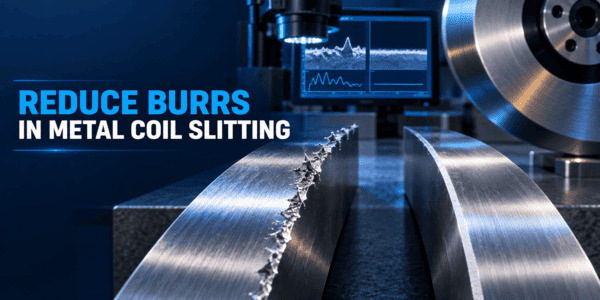
Burrs on slit metal edges can damage downstream tooling, reduce forming accuracy, create handling hazards and increase scrap. A dull circular slitter knife may be involved, but burrs usually reflect the complete slitting system. In rotary shear slitting, upper and lower knives deform the strip and guide it toward fracture. A finished edge normally contains rollover, a burnished zone, a fracture zone and a small burr. The goal is to keep burr height within specification and consistent across every lane.
Quick answer: Match knife clearance and overlap to the coil, maintain sharp and concentric tooling, stabilize the line and measure the result after each controlled adjustment.
1. Read the Slit Edge Before Changing the Setup
Inspect both sides of representative str...



 English