


Circular slitter knives are small components with an outsized influence on production. In a paper mill, flexible-packaging plant, adhesive-tape converting line, battery-foil facility or metal service center, the blade is where machine geometry, material behavior and product quality finally meet. A knife that is sharp but dimensionally unstable can create the same commercial problems as a visibly dull knife: burrs, dust, web breaks, edge wave, poor winding, frequent stoppages and rejected rolls.
That is why the most useful way to select circular slitter knives is not to ask, “Which steel is hardest?” or “Which blade lasts longest?” The better question is: Which knife material, geometry, tolerance and slitting configuration can produce the required edge quality at the required speed, with acceptable maintenance cost and process stability?
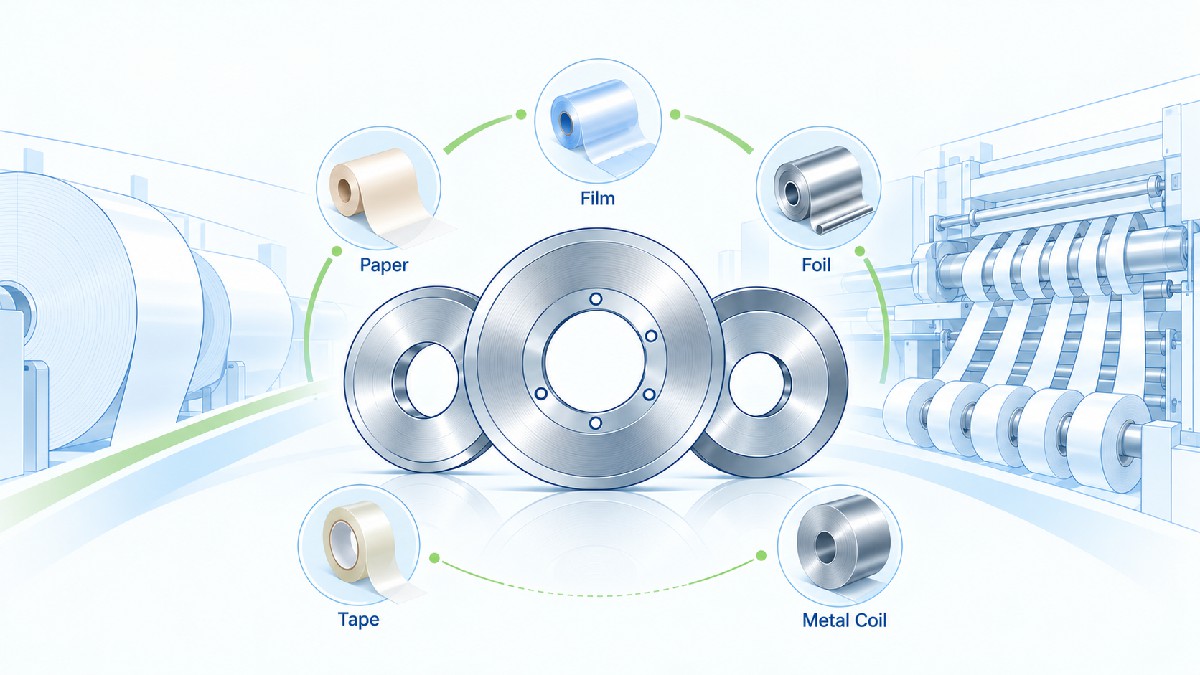
This guide is written for purchasing managers, maintenance engineers, slitter operators, OEMs and production engineers who need to specify or replace circular slitter blades, rotary slitter knives, top and bottom knives, ring knives and related tooling. It covers the selection logic for paper, board, plastic film, laminates, labels, adhesive tape, aluminum foil, copper foil, nonwovens and thin metal coil.
GUANG CHUAN manufactures industrial machine knives in Ma'anshan, China and supplies precision slitting tools for paper, plastic film, metal foil and adhesive-tape applications. Buyers who already know their dimensions can review the Circular Slitting & Rewinding Blades range; buyers working from drawings, samples or uncertain material specifications can also use GUANG CHUAN's custom blade engineering service to define geometry, material and inspection requirements before production.
Quick selection rule: Choose the cutting method first, the substrate second, the edge geometry third and the blade material fourth. Then verify flatness, runout, bore fit, thickness, overlap, side clearance and holder condition as one system. A premium material cannot compensate for incorrect slitting geometry.
Circular slitter knives are rotating cutting tools used to divide a wide web, sheet or coil into narrower strips. In many industrial applications, one upper knife works against a lower knife or anvil ring to create a controlled shear. In other systems, a razor-type blade penetrates a thin web, or a score knife presses material against a hardened roll.
The phrase circular saw blade is sometimes used loosely in industrial catalogs for any round blade. Technically, however, a saw blade normally has teeth and removes material through a repeated cutting action, while a circular slitter knife may have a smooth, sharpened circumference and separates material through shear, penetration or scoring. For paper converting, film slitting, foil processing and metal coil slitting, “circular slitter knife,” “rotary slitter knife” and “slitting knife” are usually the more precise terms.
A typical slitting system can include:
The blade therefore cannot be specified in isolation. The same nominal 100 mm or 200 mm knife can behave very differently depending on its thickness tolerance, bevel, holder stiffness, side load, overlap, arbor runout and the material being cut.
A clean slit is created when stress is concentrated at the cutting line in a controlled way. For shear slitting, the top and bottom knives behave like continuously rotating scissors. The material first experiences elastic and plastic deformation, then fracture. In metal slitting, the finished edge often shows rollover, a burnished zone, a fracture zone and a burr. In paper and film, the equivalent quality indicators are fiber pull, dust, edge fuzz, stretch, tearing, heat marks and adhesive pickup.
The industrial knife specialist DIENES identifies several relationships that directly affect shear quality, including blade profile, cant angle, overlap and dimensional runout. Its technical discussion of shear cutting quality is useful because it reinforces a point that purchasing teams sometimes overlook: sharpness is necessary, but it is not the only variable that determines a good slit.
For process engineers, it is helpful to separate the cutting system into four groups of variables:
| Variable group | Examples | What it changes |
|---|---|---|
| Knife geometry | OD, ID, thickness, bevel, dish, edge radius | Cutting force, contact area, edge stability |
| Material properties | D2, HSS, carbide, stainless grades | Wear rate, toughness, corrosion resistance, regrindability |
| Machine setup | Clearance, overlap, cant angle, side force, overspeed | Fracture behavior, heat, dust, burr, blade life |
| Substrate behavior | Thickness, tensile strength, ductility, abrasiveness, coating, adhesive | Required force, wear mode, risk of tearing or deformation |
This systems view is important commercially. A blade that costs 40% more but doubles the stable production interval can reduce total cost. The opposite is also true: an expensive carbide knife can become a poor investment if the machine has excessive runout or frequent shock loading that chips a brittle edge.
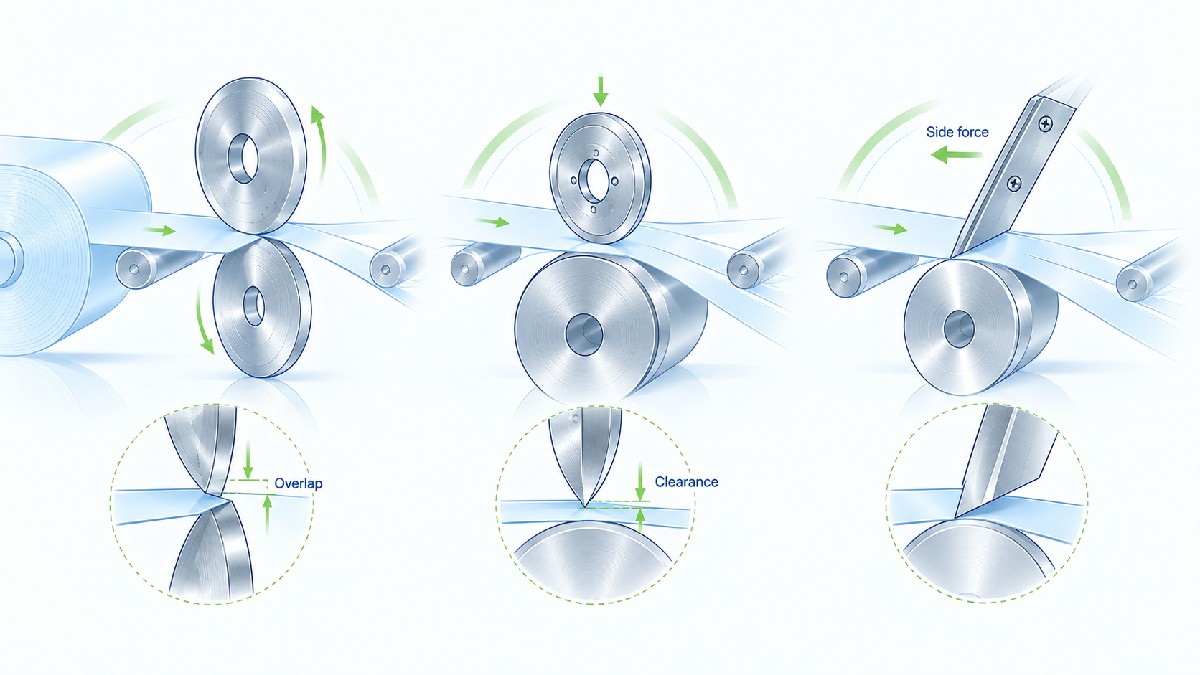
This is the classic configuration for high-quality web and coil slitting. An upper knife overlaps and contacts a lower knife or ring. The pair creates a shearing action, and the slit quality depends heavily on side clearance, overlap, cant angle, sharpness and rigidity.
Shear slitting is widely used for:
For customers using a paired upper/lower arrangement, GUANG CHUAN's industrial top and bottom slitter knives for paper converting machinery illustrate the typical specification items buyers should provide: material grade, outside diameter, inside diameter, thickness, edge geometry, flatness, runout and any special treatment.
A dished knife has a controlled offset or concavity that helps create side contact at the cutting edge while reducing unnecessary rubbing behind the cut point. Dish designs are common in certain shear-slitting holders for film, paper and foil. The exact dish, thickness and bevel must match the holder and bottom knife geometry.
Dished knives should not be copied only from outside dimensions. If the original blade has a specific dish height, spring characteristic or edge profile, the replacement should reproduce those functional dimensions. For reverse engineering, a physical sample plus the machine model can be more informative than a simple OD/ID sketch.
Flat circular knives are used where the holder or shaft arrangement provides the required side loading or where a rigid flat blade is preferred. They can be single-bevel, double-bevel or hollow-ground depending on material and cutting method.
Flat knives are often selected for:
GUANG CHUAN's 250 mm circular slitting blades for BOPP and masking tape rolls are an example of large-diameter flat rotary knives supplied in HSS or tool-steel grades for continuous converting operations.
Ring knives have a relatively large central opening and may be used in paper core cutting, tube cutting, web slitting and other rotary applications where the blade mounts over a large hub or support. In this design, bore accuracy and concentricity become especially important because any eccentricity is magnified during rotation.
When specifying a ring knife, include:
Some slitters use lower knives with multiple precision grooves or cutting lands. These designs can support multi-lane production and reduce assembly complexity, but groove pitch, land width, concentricity and surface finish must be controlled carefully. GUANG CHUAN manufactures multi-groove multi-edge bottom slitter rotary blades for foil, paper, adhesive substrates and composite materials.
Razor slitting uses a very sharp thin blade to penetrate flexible webs such as film. Score or crush slitting presses a blade against a hardened roll and separates material through compression and localized fracture. These methods can be economical and fast, but they should not automatically be treated as substitutes for shear slitting.
The table below provides a practical first comparison.
| Slitting method | Typical materials | Main advantages | Main limitations | Typical knife/tool form |
|---|---|---|---|---|
| Shear slitting | Paper, board, film, foil, thin metal, labelstock | High edge quality, good control, suitable for many thicknesses | More setup-sensitive; requires top/bottom alignment | Circular top knife + bottom knife/anvil |
| Razor slitting | Thin plastic film, some laminates | Low equipment complexity, low cutting force | Blade wear can be fast; less suitable for thick/abrasive webs | Thin razor blade or rotary razor |
| Score/crush slitting | Paper, nonwoven, some films | Simple setup, robust for selected webs | Can compress or deform edge; anvil wear matters | Score wheel against hardened roll |
| Hot slitting | Thermoplastic textiles/films | Can seal edges while cutting | Heat control and fumes; not suitable for all substrates | Heated knife or wheel |
For buyers, the practical message is simple: do not choose a blade material before confirming the slitting method. The mechanical load on a shear knife is different from the load on a score knife, and the “best” steel changes accordingly.
Two knives made from the same steel can deliver very different results if their edge profiles differ. Edge geometry determines how cutting force is concentrated, how much material contacts the blade, how well the edge resists chipping and how easily the blade can be resharpened.
A single-bevel knife has one primary cutting face and one flatter reference face. It is common in shear-slitting systems where the bevel direction is designed to work against a mating bottom knife. Single-bevel profiles can provide a strong, controlled edge and help manage material displacement.
The specification must identify bevel orientation. “Single bevel, 30°” is incomplete if the drawing does not show which face is beveled and how the knife is mounted.
Double-bevel knives sharpen from both sides and can be useful where a symmetric profile reduces directional effects. The included angle influences both sharpness and edge strength. A smaller angle penetrates more easily but leaves less material supporting the edge. A larger angle is stronger but may require more force.
Hollow grinding reduces contact behind the cutting edge. In adhesive or heat-sensitive slitting, lower contact area can reduce drag and buildup. DIENES, for example, notes in its discussion of adhesive buildup on slitter blades that profile changes can help reduce material contact in some shear-cut applications.
A newly ground edge is not infinitely sharp. Under magnification, it has a finite edge radius and a ground surface texture. A very fine edge can improve initial cut quality, but excessive fragility can create micro-chipping on abrasive or impact-loaded materials. The optimum finish is therefore application-specific.
For procurement, it is more useful to specify the required cut result and process conditions than to demand “mirror polish” without context. Surface polish, edge radius, coating and cleaning behavior should be matched to the substrate.
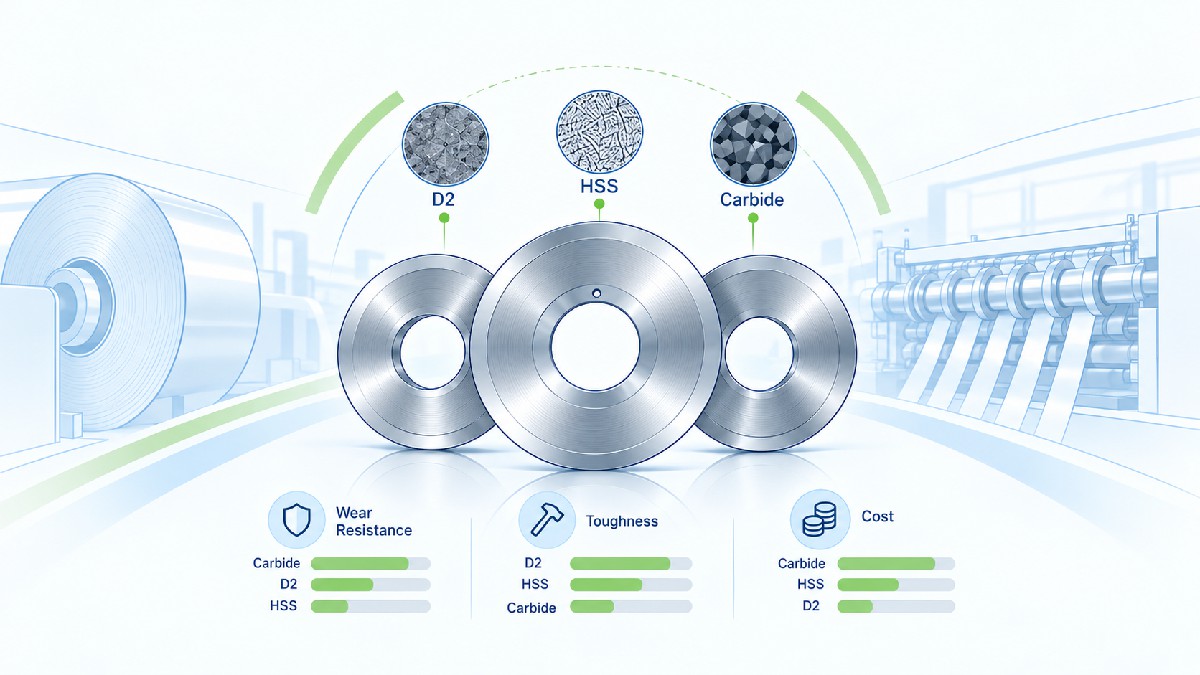
Material selection is one of the most searched topics because it directly affects wear life, regrinding interval and price. However, hardness alone is not an adequate selection criterion. The blade must balance:
International standards help establish a common language. ASTM A681-24 covers alloy tool steels, while ASTM A600 covers high-speed tool steels including M-series grades. ISO 4957:2018 also defines requirements for cold-work, hot-work and high-speed tool steels and remains current after review in 2023.
D2 is a high-carbon, high-chromium cold-work tool steel widely used for industrial knives because it combines strong wear resistance with reasonable dimensional stability and manageable cost. Uddeholm describes AISI D2 as a high-wear-resistance cold-work steel and lists a typical hardened range around 60-62 HRC for its grade information.
D2 is often a practical choice for:
D2 is not automatically identical to every material sold as “SKD11.” JIS SKD11 and AISI D2 are close equivalents in many commercial contexts, but procurement drawings should specify the accepted standard or chemistry rather than rely only on an informal equivalent name.
M2 is one of the most widely used molybdenum high-speed steels. It provides higher hot hardness and strong edge stability compared with many conventional cold-work tool steels. Griggs Steel's high-speed steel composition chart lists typical M2 chemistry and a tempered hardness around 64 HRC, while BÖHLER's S600 / 1.3343 / HS6-5-2C is an M2-type HSS positioned for high wear resistance, edge stability and hot hardness.
M2 is a strong candidate when:
M42 contains cobalt and is known for high hot hardness and high achievable hardness. Griggs lists a typical tempered value around 67 HRC for M42. This can be useful in high-speed or high-temperature cutting, but higher hardness and alloy content increase cost and can reduce tolerance to shock or abusive setup.
M42 should be considered when the process has demonstrated a genuine thermal or wear limitation with M2, not simply because a higher HRC number appears better on a datasheet.
Cemented tungsten carbide can provide outstanding wear resistance. Its properties vary substantially with carbide grain size, binder percentage and grade design. Hyperion's carbide property data show representative cutting grades with hardness values roughly in the 1,400-1,900 HV30 range, while tougher grades sacrifice some hardness for higher fracture resistance. This is why “tungsten carbide” should never be treated as one universal material.
Carbide is often justified for:
Carbide's disadvantage is brittleness relative to tool steel. If the holder jumps, the arbor has excessive runout or foreign material enters the cut, chipping can be expensive. A tougher carbide grade may outperform a harder grade in such conditions.
For food-contact, humid or chemically aggressive environments, corrosion resistance may outweigh maximum wear resistance. Martensitic stainless steels such as 420- or 440-series grades can be used in selected circular knife applications. Their selection should be based on hygiene, corrosion exposure, required hardness and cleaning chemistry rather than a generic preference for “stainless.”
The values below are selection-oriented ranges and typical published data, not universal guarantees. Final hardness should be tied to the exact grade, heat-treatment route, blade thickness and supplier specification.
| Material family | Typical hardness reference | Relative wear resistance | Relative toughness | Best fit | Procurement note |
|---|---|---|---|---|---|
| D2 / 1.2379 / SKD11-type | commonly around 58-62 HRC in industrial knife use | High | Medium | General paper, film, tape, foil, thin metal | Strong cost/performance baseline; verify standard and heat treatment |
| M2 HSS / 1.3343 | about 64 HRC typical in published HSS data | Very high | Medium-high | High-speed, abrasive converting, repeated production | Better hot hardness and edge stability than many cold-work steels |
| M42 HSS | about 67 HRC typical in published HSS data | Very high | Medium | High thermal load and demanding wear | Higher cost; confirm need for cobalt HSS |
| Cemented tungsten carbide | often ~1,400-1,900 HV30 depending on grade | Exceptional | Grade-dependent, generally lower impact tolerance than steel | Ultra-long runs, abrasive films/foils, high precision | Specify carbide grade, binder, grain size and chipping risk |
| Martensitic stainless steel | grade-dependent | Medium | Medium | Food, wet or corrosive environments | Select for corrosion plus required hardness, not corrosion alone |
Two D2 knives from different suppliers can show very different service life because steel grade is only one part of the manufacturing route. Heat treatment controls hardness, retained austenite, carbide condition, residual stress and dimensional stability. Grinding quality after heat treatment also determines whether the edge contains thermal damage or grinding cracks.
A professional blade manufacturing route may include:
BÖHLER's tool-grinding guidance explains that high-alloy tool steels and HSS become more difficult to grind as carbide content and wear resistance increase. Poor grinding parameters can introduce heat damage or cracks. For buyers, this is an important reminder that a material certificate does not replace finished-tool inspection.
GUANG CHUAN states on its service page that it combines precision CNC manufacturing, hardness control, high-precision grinding and multi-point inspection. When requesting a quote, buyers should still define the actual acceptance values required by their machine, especially for runout, flatness, parallelism and bore fit.
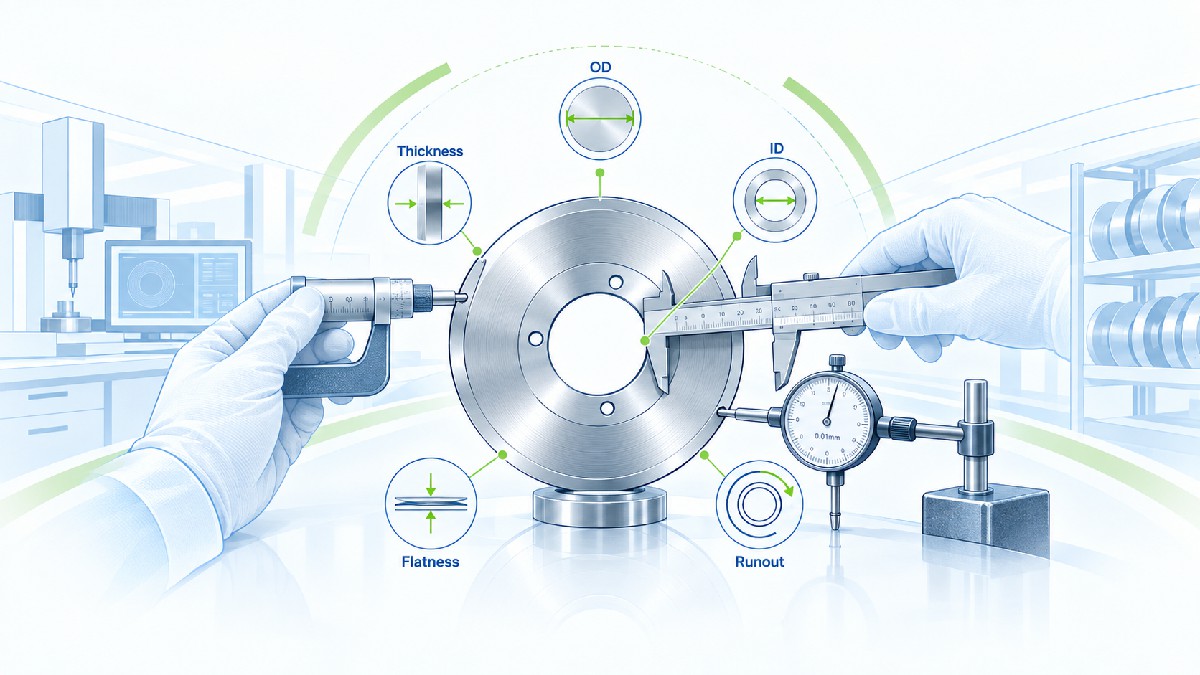
For circular slitter knives, dimensional accuracy can be as important as hardness. A blade that is only 0.01 mm wrong in the wrong feature may create more trouble than a several-point difference in HRC.
OD affects surface speed, overlap geometry, usable regrind allowance and compatibility with guards and holders. Matched knife sets may need tightly controlled diameter variation so that each lane engages consistently.
When replacing an existing blade, record both the original nominal OD and the current worn OD. A repeatedly reground sample may be significantly smaller than the original specification.
The bore establishes the blade's position relative to the shaft or hub. Excessive clearance can produce eccentricity and vibration; an overly tight fit can make installation difficult or introduce distortion. Drawings should state the bore tolerance and, where applicable, keyways, drive pins, bolt circles or locating shoulders.
Thickness affects stiffness, lane spacing and cut geometry. In shear slitting, very small thickness errors can change side contact and spacer-stack dimensions. If knives are used with precision spacers, specify actual finished thickness tolerance rather than only nominal thickness.
Flatness and parallelism influence how a knife contacts the mating tool. A warped blade may touch intermittently, increasing heat, noise, wear and inconsistent edge quality. GUANG CHUAN lists example circular-slitter product tolerances in the micron range on several product pages, including its top and bottom slitter knives. Those values should be treated as product-specific capability examples; the drawing for each order should define the acceptance requirement.
Radial runout causes the cutting edge to move in and out as the blade rotates. Axial runout causes side-to-side movement. Either can create cyclic changes in overlap, side force and effective knife position. DIENES specifically identifies runout as a factor that can increase wear and reduce slitting stability.
ISO 1101:2017 provides the international geometrical tolerancing language for form, orientation, location and runout. Using recognized GD&T notation on blade drawings makes supplier communication much clearer than phrases such as “very precise” or “no wobble.”
| Feature | Why it matters | Recommended way to specify |
|---|---|---|
| OD | Surface speed, overlap, regrind life | Nominal size + tolerance |
| ID | Concentric mounting | Fit/tolerance class or explicit limit |
| Thickness | Stiffness and spacer stack | Finished thickness + tolerance |
| Flatness | Stable side contact | GD&T flatness value |
| Parallelism | Uniform thickness/side face relationship | Parallelism to datum face |
| Radial runout | Edge concentricity | Total or circular runout relative to bore datum |
| Axial runout | Side-face stability | Face runout relative to bore/axis |
| Bevel angle | Cutting force and edge strength | Angle + orientation + tolerance |
| Surface finish | Friction, adhesive pickup, sealing behavior | Ra/Rz where functionally required |
| Hardness | Wear/toughness balance | HRC/HV range + test location if critical |
Paper looks easy to cut, but high-speed paper slitting is demanding because fiber, fillers and coatings create abrasion while the customer expects clean edges with minimal dust. The wrong overlap or excessive side load can accelerate dulling even when the knife material is adequate.
Valmet's practical guide to slitter adjustments gives useful reference values for paper applications. For its equipment, recommended blade/band overlap increases from less than about 0.030 inch for tissue to roughly 0.060-0.080 inch for heavier board and liner grades. These are machine-specific reference values, not universal settings, but they demonstrate how strongly substrate grade changes the required setup.
For paper and board, buyers should prioritize:
GUANG CHUAN's HSS circular cardboard slitting blades are designed for corrugated and paperboard converting where wear resistance and stable high-speed cutting are important.
Film slitting is sensitive to blade sharpness, web tension, heat and drag. Thin film can stretch around a dull edge instead of fracturing cleanly. Heat-sensitive materials can show fused or deformed edges. Laminates may include abrasive print layers, coatings or fillers that shorten knife life.
Key questions are:
For thin flexible films, lower-friction profiles and extremely sharp edges are often more important than maximum bulk hardness. M2 HSS or carbide can be justified when the line speed and abrasive content cause D2 to dull too quickly.
Adhesive creates a different failure mode: buildup. As adhesive transfers to the knife, drag increases, heat rises and the web may wander or tear. A blade can still be “sharp” and yet perform poorly because the side face is contaminated.
For BOPP tape, masking tape, double-sided products and labelstock, consider:
GUANG CHUAN's 250 mm BOPP and masking tape slitter blades provide a relevant reference for large-diameter tape-converting knives.
Foil is thin but unforgiving. Small knife defects can produce burrs, edge waves or particles that matter in capacitor, electronics and battery applications. Copper foil is also abrasive enough to challenge ordinary tool steels in continuous production.
For precision foil slitting, evaluate:
A useful rule is that the thinner the foil and the tighter the quality requirement, the more important geometry and concentricity become. Simply moving from D2 to carbide without fixing arbor runout or spacer accuracy may not improve the result.
Metal coil slitting uses much higher forces than flexible-web slitting. Horizontal knife clearance, vertical penetration, spacer stack accuracy, strip tensile strength and ductility all influence the fracture pattern.
GUANG CHUAN's technical article on reducing burrs when slitting metal coils explains why burr should be diagnosed from the full system rather than blamed automatically on dull knives. For heavy metal applications, the knife grade must also tolerate compressive load and occasional shock.
For purchasing teams, a quote request should include:
Nonwovens can be soft, fibrous, abrasive or thermoplastic. A blade that works well on spunbond polypropylene may not be ideal for glass-fiber-containing material. The primary defects are often fuzz, pulled fibers, uncut strands and heat buildup.
Selection should focus on:
Paper cores are thick composite structures made from wound layers of paper and adhesive. They can create heavy dust and rapid abrasion. Ring knives or large-diameter HSS tools are common. The blade must cut without collapsing the tube wall or creating loose fibers that contaminate the winding process.
For core cutters, edge strength and heat resistance may justify HSS even when D2 performs acceptably on ordinary paper web slitting.
Correct knife selection can fail if the setup is wrong. Four settings deserve special attention.
In paired shear cutting, side clearance is the horizontal relationship between the upper and lower cutting edges. For metal, clearance is typically selected as a function of thickness, strength and ductility. For flexible webs, holder geometry and side force often define how the blades contact.
There is no safe universal percentage for every material. A value suitable for mild steel may be wrong for stainless, aluminum, copper or a polymer laminate. The correct approach is to begin from the slitter OEM's validated recipe, then verify the finished edge and adjust one variable at a time.
Overlap is how far the top knife passes below the tangent level of the bottom knife. Too little overlap can cause incomplete or unstable cutting; too much can increase drag, wear and dust.
DIENES explains in its article on incorrect overlap and dust generation that excessive overlap increases the distance the web travels in contact with the knife. For many flexible-web applications, it gives a general reference of approximately 0.030-0.040 inch. Again, that number is a starting reference for certain systems, not a universal specification.
Valmet gives different overlap ranges for different paper grades on its equipment, reinforcing the same point: use the minimum overlap that produces a stable, complete cut on the actual machine.
Cant angle establishes the angular relationship between the upper blade and the lower knife or band. The purpose is to maintain a defined cut point while minimizing unnecessary contact. Too much angle can accelerate wear; too little can make the cut unstable.
Knife holders are often designed around a specific cant angle. Do not modify the angle by improvising shims unless the OEM procedure permits it and the effect can be measured.
Side force keeps the top knife in contact with the lower knife in many pneumatic shear systems. More is not always better. Valmet notes that excessive side loading accelerates blade wear and recommends using only enough force to maintain proper cutting and drive. This principle is broadly useful even though exact force values remain machine- and substrate-specific.
The table below summarizes typical symptoms.
| Symptom | Possible setup cause | What to check first |
|---|---|---|
| Heavy dust/fuzz | Excessive overlap, dull blade, wrong profile | Verify overlap, edge condition and cut point |
| Rapid edge wear | Too much side force, excessive overlap, poor runout | Reduce force to validated minimum; check holder and arbor |
| Knife jumping | Too little overlap or unstable holder | Check engagement, air pressure, runout and holder condition |
| One lane has defects | Local knife/spacer/holder problem | Inspect that pair before changing the entire line |
| Edge heats or adhesive builds up | Excessive contact area, poor finish, contamination | Check profile, polish, cleaning method and side load |
| Burr cycles once per revolution | Radial/axial runout | Measure blade, shaft, spacer and mounting faces |
Circular knives are rotating components, so safe operation must consider both line speed and rotational speed. Surface speed can be calculated from knife diameter and RPM:
Surface speed (m/min) = π × knife diameter (m) × RPM
For example, a 200 mm knife rotating at 1,000 RPM has a circumference of approximately 0.628 m and a surface speed of about 628 m/min.
This simple calculation is useful when a customer changes blade diameter. A larger knife at the same RPM has a higher surface speed and may change heat generation, balance requirements and holder behavior. When the lower anvil is driven, some systems intentionally run it slightly faster than the web. A current Tidland/Maxcess knifeholder manual recommends, for that specific system, driven-anvil overspeed around 3-5% above winder speed when troubleshooting certain slit issues. Such values should only be used within the OEM's approved setup range.
For large-diameter knives or very high RPM, ask the supplier about dynamic balance and maximum safe speed. A blade drawing should never be approved for high-speed use solely because the dimensions match.
A structured selection process reduces trial-and-error and makes supplier quotations easier to compare.
Confirm whether the machine uses shear, razor, score/crush or another method. Photograph the holder and knife arrangement if the terminology is unclear.
Record the actual material, not only a trade name. For metals, include grade, temper and strength where available. For film, include resin type, layers, thickness and fillers. For paper, include basis weight, coating and abrasive additives.
What does the customer reject?
A blade should be optimized for the defect that matters commercially.
Provide manufacturer, model, holder type, arbor diameter, blade mounting method and any OEM part number. If the machine is old or modified, send photos and measurements.
Do not assume the old knife still represents the original dimensions. Measure OD, ID, thickness, mounting features and bevel. If the knife has been reground many times, ask whether an older drawing or unused sample exists.
Start with the current grade. If performance is acceptable, replacing it with the same or an equivalent verified grade is low risk. Upgrade to HSS or carbide only when the economics or process requirement justify it.
Specify single/double bevel, angle, dish, hollow grind and edge orientation. If the existing profile works well, replicate it before experimenting with a new one.
Use measurable drawing values for flatness, runout, bore, thickness and OD. Do not over-tolerance noncritical features: unnecessary microns increase manufacturing cost without improving cut quality.
Install the knife using the machine's approved procedure. Record overlap, side force, clearance, cant angle and line speed. Change one variable at a time during trials.
The cheapest knife is not always the lowest-cost knife. Consider:
A blade that costs twice as much but runs four times longer may be less expensive in a 24-hour production line. Conversely, a premium carbide knife can be wasteful on a low-volume machine that changes products frequently and never uses the potential wear life.
Buyers can compare two knife options with a simple cost-per-production-hour or cost-per-million-meters model.
Assume:
The downtime cost per change is:
1.5 × $350 = $525
If the knife set is reground three times before replacement, a simplified lifecycle cost is:
$600 + (3 × $180) + (4 × $525) = $3,240
Now assume an HSS set costs $1,000 but doubles the interval to 600 hours while keeping the same number of regrinds. Even though the purchase price is $400 higher, the number of blade changes across the same production horizon can be much lower. The savings may come primarily from avoided downtime rather than steel price.
This example is intentionally simplified. A real model should also include scrap, labor, freight, interest on inventory and the effect of quality complaints. The purpose is to prevent procurement decisions based only on the invoice price of the knife.
Possible causes include normal edge wear, abrasive material, pickup, incorrect clearance, increased temperature or unstable side loading. Compare the first roll and later rolls under the same setup. If all lanes degrade together, suspect a system variable or uniform wear. If one lane degrades, inspect that knife pair and spacer stack.
High hardness does not prevent chipping; it can increase chipping risk when toughness is insufficient. Check for knife contact during engagement, excessive side load, foreign particles, holder looseness, arbor runout and brittle material selection. A slightly tougher HSS or carbide grade may outperform the hardest available grade.
In shear slitting, the two edges can show different rollover/fracture characteristics if clearance, bevel orientation or knife alignment is wrong. Confirm that top and bottom knives are installed in the correct direction and that the spacer stack is accurate.
A new edge can still generate dust if overlap is excessive, the web path is unstable or the blade profile creates too much contact. DIENES specifically warns about excessive overlap in dust generation. Verify setup before replacing the knife again.
Check blade sharpness, web tension, guiding, holder rigidity and heat. A flexible film can be displaced by a dull edge or excessive contact instead of being cut. Wrinkles may originate upstream and only become visible at the knife.
Check blade finish, profile, coating compatibility, line temperature and cleaning method. Do not use an aggressive cleaning chemical that attacks the coating or substrate without supplier approval.
Investigate incoming substrate abrasiveness, coating, hardness, filler content and contamination. Also verify that replacement knives truly share the same steel grade, heat treatment and edge finish. A purchasing description such as “D2, 60 HRC” does not fully define the product.
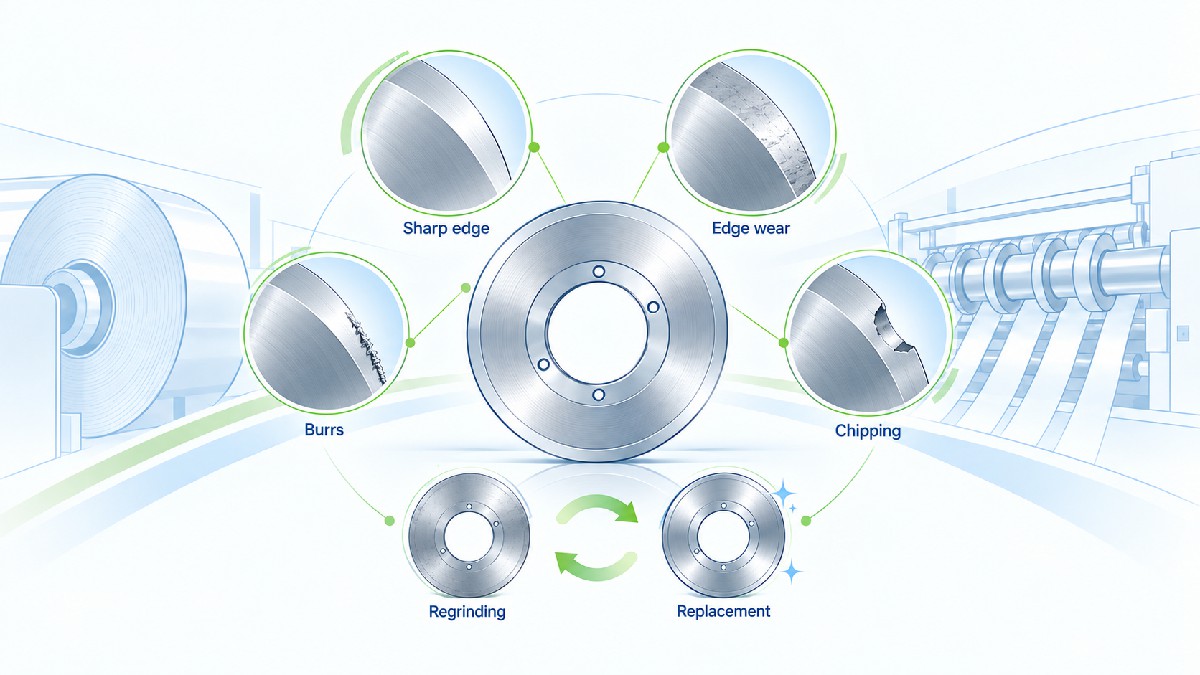
Circular slitter knives are often resharpenable, especially tool-steel and HSS designs. The goal of regrinding is to restore the specified edge while removing as little material as possible and maintaining concentricity, flatness and matched diameter.
GUANG CHUAN's guide on when circular slitter knives should be resharpened or replaced recommends evaluating the full knife condition rather than replacing a blade only because cut quality has declined.
A knife is a good regrind candidate when:
Replacement is normally safer when:
Matched top/bottom sets may need coordinated regrinding. If one knife becomes much smaller than neighboring knives, engagement and overlap can vary lane to lane.
Safety is equally important. Knife changes expose workers to sharp edges and hazardous machine energy. In the United States, OSHA's 29 CFR 1910.147 lockout/tagout standard establishes requirements for controlling hazardous energy during servicing and maintenance. Local regulations and the slitter manufacturer's procedures should always govern the actual changeover process.
The fastest way to receive an accurate technical quotation is to provide enough information for the supplier to reproduce the functional blade, not just its diameter.
| RFQ item | Example |
|---|---|
| Application | BOPP tape slitting / copper foil / coated paper / stainless strip |
| Machine | Manufacturer + model |
| Knife type | Top knife, bottom knife, ring knife, multi-groove knife |
| OD | 200.000 mm |
| ID | 120.000 mm H7 or stated tolerance |
| Thickness | 3.000 mm ±0.003 mm |
| Edge | Single bevel 30°, right-hand orientation |
| Material | D2, M2 HSS, carbide grade, or “supplier recommendation” |
| Hardness | Required HRC/HV range if known |
| Flatness/runout | Drawing values |
| Material being cut | PET 25 μm laminate / SS304 0.5 mm, etc. |
| Line speed | m/min |
| Current problem | Burr, dust, short life, chipping, adhesive buildup |
| Quantity | Trial set + annual demand |
If no drawing is available, GUANG CHUAN's OEM/ODM service accepts technical drawings or physical samples for replacement development. For a worn sample, include the machine model and explain whether the knife has been reground; this helps avoid copying a reduced OD as if it were the original design.
A professional drawing should include enough information to prevent assumptions. For simple knives, that may be only one page. The essential features are:
For complex or high-speed tools, add balance requirements and maximum operating speed. If the drawing uses GD&T, reference datums clearly so the inspection method is unambiguous.
Custom tooling is justified when a standard knife creates recurring production problems or does not fit the machine properly. Common reasons include:
Custom does not necessarily mean expensive complexity. In many cases, the most valuable customization is a small change: a better bore fit, a different bevel angle, a tougher carbide grade or a tighter runout specification.
A common purchasing mistake is to treat blade life as a material-only problem. Suppose a plant has D2 knives that last only two weeks. The instinct may be to upgrade to M2 or carbide. But if the holder has excessive backlash or the arbor face contains debris, the new material may fail almost as quickly.
Before paying for a material upgrade, check:
This diagnostic approach also helps the supplier recommend the correct knife. A statement such as “our D2 blade life is poor” gives little engineering information. A better statement is: “We slit 18 μm PET/Al/PE laminate at 450 m/min; dust rises after 120 hours; current knife is D2 at 60-61 HRC; radial runout measured at 0.008 mm; overlap is 0.8 mm.” That data allows a meaningful technical response.
GUANG CHUAN's About Us page describes a manufacturing base equipped with CNC machining centers, grinding equipment and heat-treatment capability for industrial blades. Its slitting portfolio covers paper, plastic film, metal foil, adhesive tape and related converting applications.
Depending on the application, available solutions can include:
For customers comparing a current knife with an upgraded material, it is useful to send one worn blade, one unused blade if available, recent cut samples and the production history. This allows geometry and wear mode to be evaluated together.
A circular saw blade normally has teeth and cuts by repeated tooth engagement, while a circular slitter knife often has a continuous sharpened edge and cuts by shear, penetration or scoring. The correct term for paper, film, foil and many coil-slitting applications is usually circular slitter knife or rotary slitter knife.
Neither is universally better. D2 is a strong general-purpose choice with good wear resistance and economical regrinding. M2/M42 HSS offers higher hot hardness and often better edge stability for high-speed or abrasive applications. The correct choice depends on substrate, speed, holder condition and required maintenance interval.
Carbide is most attractive when wear is the dominant failure mode and the machine is stable enough to avoid shock chipping. Ultra-thin foil, abrasive coated materials and long continuous runs are common candidates. Calculate savings from reduced changes and scrap rather than comparing purchase price alone.
There is no universal value. Many D2 industrial knives are supplied around 58-62 HRC, M2 is commonly used around the low-to-mid 60s HRC and cobalt HSS can be higher. Carbide is normally specified by grade and Vickers/Rockwell A hardness rather than HRC. Hardness must be balanced with toughness.
Use the slitter manufacturer's specification. DIENES gives approximately 0.030-0.040 inch as a general reference for many flexible-web applications, while Valmet shows different ranges by paper grade on its systems. The practical goal is the minimum overlap that maintains a stable complete cut without excessive drag.
New blades can still produce dust if overlap, cut point, side force, cant angle, web tension or blade profile is wrong. Check system geometry before assuming the new knife is defective.
Yes, many tool-steel and HSS knives can be reground multiple times if they remain flat, crack-free and within minimum OD/thickness limits. Record the amount removed at each grind.
Common causes include knife-to-knife collision, excessive side load, insufficient toughness, foreign particles, holder play, incorrect overlap and arbor runout. Carbide and very hard HSS require especially stable setup.
Mount the blade on an appropriate inspection arbor or fixture and use a dial indicator at the cutting edge for radial runout and on the side face for axial runout. The measurement datum and clamping method should match the drawing. For critical parts, define runout with recognized GD&T practice such as ISO 1101.
A drawing is best. If unavailable, provide a sample, machine model, OD, ID, thickness, bevel details, material being cut, line speed, current blade material and the problem you want to solve. GUANG CHUAN can manufacture custom industrial blades from drawings or samples.
Before issuing a purchase order, confirm all of the following:
The best circular slitter knife is not the one with the highest hardness number or the lowest quotation. It is the knife that produces a stable cut for the required substrate, works correctly with the holder and machine geometry, can be inspected and maintained predictably, and delivers the lowest total cost over its useful life.
For paper, film, foil, tape and metal-converting applications, explore GUANG CHUAN's Circular Slitting & Rewinding Blades, or send your drawing and production conditions through the custom blade engineering service for a material and geometry recommendation.

Leave A Message
Scan to WhatsApp :
 English